Client Packaging Projects: From Sampling to DDP Delivery

Real custom packaging produced for jewelry, cosmetics, electronics, food and e-commerce brands — see what our factory makes for clients worldwide.

  • 20+ years of packaging printing expertise
  • 5,000 m² factory with Heidelberg Speedmaster CD102 5-color offset presses
  • ISO 9001 / FSC / SEDEX / RoHS certified
  • ΔE≤2 color accuracy on every batch
  • 500 pcs MOQ with 3-8 day sampling

The cases below describe production problems we ran into and how we traced them — a fold that cracked, a carton that sprang open, colour that drifted across a long run. Each case is written in the same order: the client type and what failed on the line, the root cause we traced in the material or the die, the exact parameter changes we made, and the measured result after the fix.

The figures come from our own production reviews: press sheets, QC logs and the sample library kept for every order. Client names stay confidential, so cases are described by product type, board grade, structure and quantity. If your project resembles one of them, quote the case number in your enquiry and we will start from the parameters that already worked.

Three production problems, and the parameters that fixed them

Real technical post-mortems from our sample room and press floor — problem, root cause, solution, measured result.

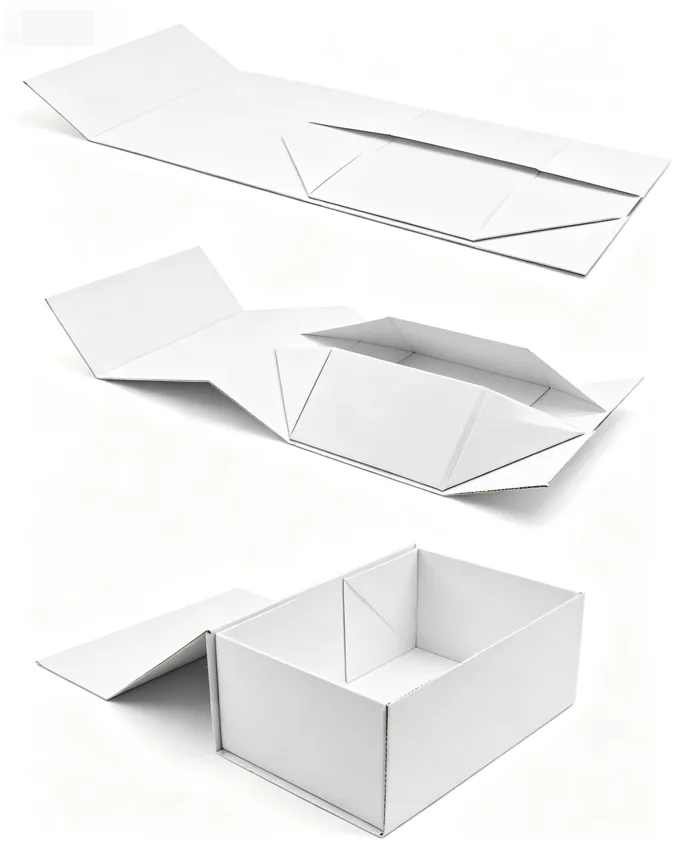
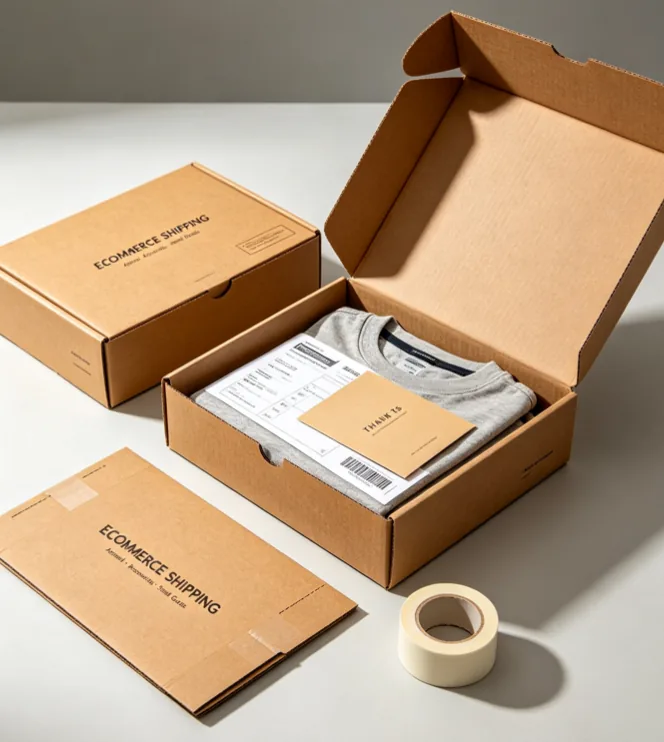
One-piece folding e-commerce shipping mailer box assembled on our sample bench, the same mailer structure used in case 1

Case 1 — Premium cosmetics mailer: cracked corners at 14.2%

Client type
Premium beauty brand gift-set mailer: 250 gsm white-lined grey board facing paper laminated over E-flute corrugated board.
The problem
When the three-ply side wall was folded through a full 180°, the facing paper and the ink layer cracked open and exposed the corrugated fibres underneath. 14.2% of the run was rejected. The lid also sprang back and would not self-lock, and the crease lines delaminated during folding.
Root cause
Three measurable causes: the crease line was too narrow to crush the flute peaks, so the board had nowhere to go at the fold; the crease ran with the flute direction, which makes the board stiffer across the bend; and winter workshop humidity sat at only about 35% RH, dropping board moisture below 6% so the fibres turned brittle before they ever reached the die-cutter.
How we solved it
The single crease line became twin crease lines set 2.0 mm apart. The creasing rule was changed to a 6 pt rounded rule and the crease channel was widened to 4.0 mm. Before die-cutting, board is conditioned with a water spray so the workshop holds 55%–65% RH and moisture returns to 8%–10%.

Delivery result

Corner cracking fell from 14.2% to 0%. Fold resistance dropped 55%, and packers now close and self-lock the mailer by hand with no tools or jigs.

  • 14.2% → 0% corner cracking
  • −55% fold resistance
  • Hand self-lock, no tools

Die-cut structure diagram of the one-piece folding carton from case 2, showing the fold lines and panel layout on the die

Case 2 — Consumer electronics one-piece carton: a crease set for the wrong board

Client type
Consumer electronics outer carton: one-piece folding box with auto-lock base and an integrated inner tray, folded from 350 gsm one-side coated white-lined grey board 0.46 mm thick plus 18 μm matte BOPP film.
The problem
On the automatic gluing line, the 180° main crease demanded so much torque that the robot arms slipped and the blank stalled. 18.5% of the run was rejected. Creases sprang back badly, micro-cracks appeared between the film and the paper fibres, and the lid opened on its own by 15°–20°.
Root cause
The die was still set to the parameters used for 250 gsm card stock — a 0.71 mm creasing rule with a 1.30 mm channel — which is simply too narrow for board 0.46 mm thick. On top of that, the main crease ran parallel to the paper grain in the machine direction, which raises bending resistance by nearly 40%, and the BOPP film was never pre-broken before the fold.
How we solved it
Creasing rule 0.71 → 1.05 mm (3 pt); crease channel 1.30 → 1.50 mm with a 0.50 mm channel depth. The sheet was re-imposed so the main crease runs parallel to the cross direction, cutting bending resistance by a further 35%. A 180° pre-fold wheel was added ahead of the gluer, and the inner corner and hidden creases were converted to half-cut perforations with a 1:1 depth release.

Delivery result

Validated across a 50,000-piece production run: rejects fell from 18.5% to 0.2%, bending force dropped from 4.2 to 1.6 N·cm, lid spring-back was held within 3°, edge and film cracking came in at 0%, and box corners kept a true 90° angle.

  • 18.5% → 0.2% rejects
  • 4.2 → 1.6 N·cm bending force
  • Spring-back within 3°
  • 90° corners · 0% film cracking
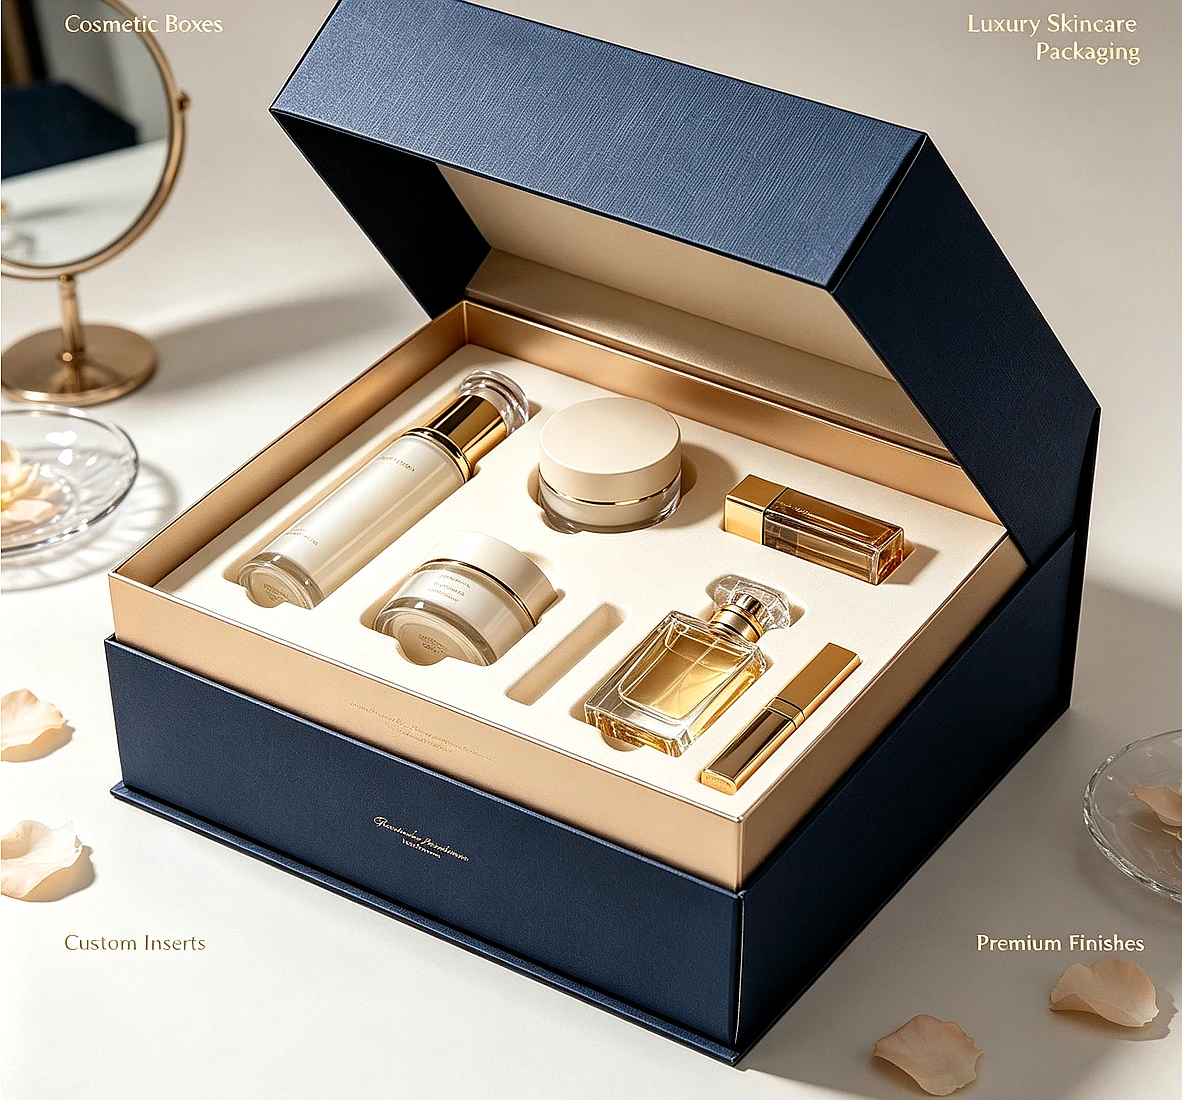
Printed cosmetic and makeup cartons from the cosmetics carton production run described in case 3

Case 3 — 100,000-piece cosmetics carton: holding ΔE within 2.0

Client type
Cosmetics brand ordering 100,000 printed makeup cartons to one design, one ink set and one delivery date.
The problem
A 100,000-piece run has to look like a single carton. Colour is the specification most likely to be questioned when the pallets are opened at the buyer warehouse, so it has to be measured rather than judged by eye.
Root cause
Colour consistency at this volume is a colour management question rather than a press question. It is held by instrument measurement, not by the operator eye: an X-Rite spectrophotometer read under D65 illumination and recalibrated every day against a standard colour patch.
How we solved it
The batch ran under our standard colour protocol — X-Rite spectrophotometer measurement under D65 illumination, instruments recalibrated daily with a standard colour patch, and every batch checked against the signed and approved proof before release.

Delivery result

Colour deviation across the whole 100,000-piece batch was held within ΔE 2.0.

  • 100,000 pcs in one batch
  • ΔE ≤ 2.0 across the batch

Which industries we actually produce for

Six categories account for most of our export orders. Each has established defaults for board, structure and finishing.

  • Jewelry & watches

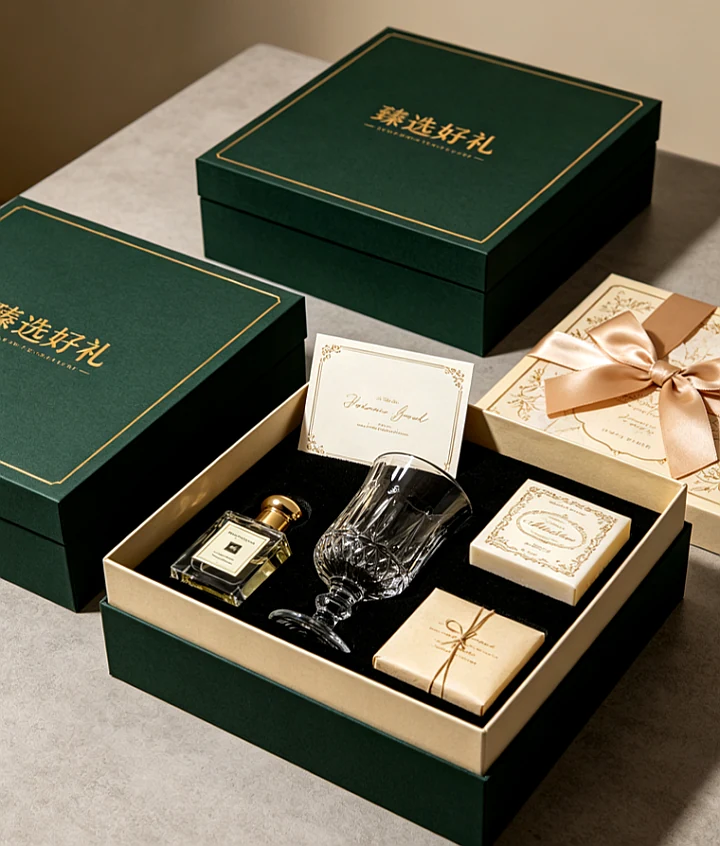
    Velvet or EVA inserts, magnetic lids and small-format rigid boxes; 500 pcs MOQ keeps a seasonal collection testable.

  • Beauty & cosmetics

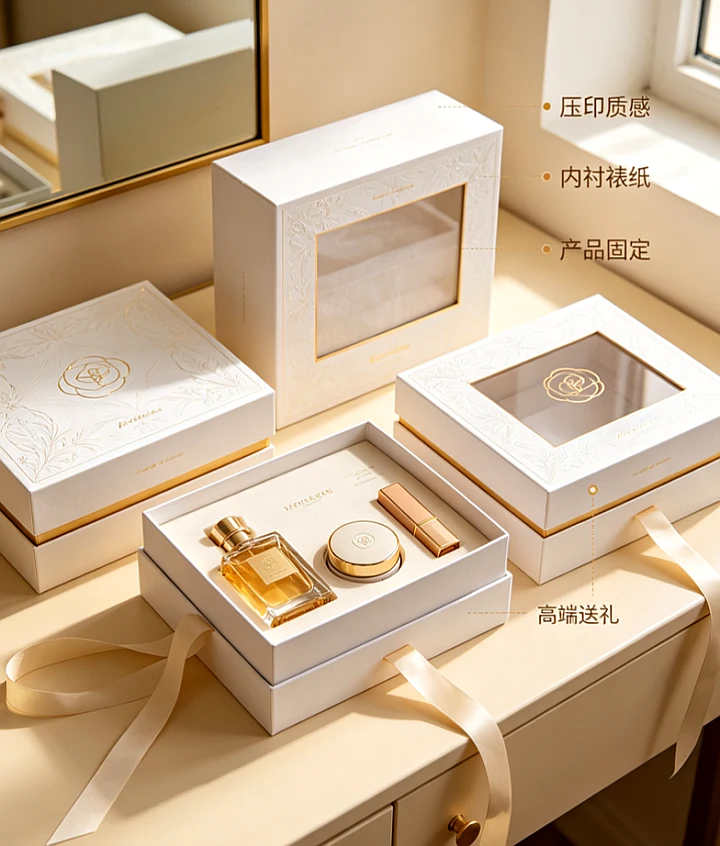
    Foil, spot UV and soft-touch on 350 gsm board, with colour held within ΔE≤2 across long runs (see case 3).

  • Consumer electronics

    Auto-lock bases, die-cut EVA cradles and RoHS-compliant inks and board for accessory packaging.

  • Tea, food & gifting

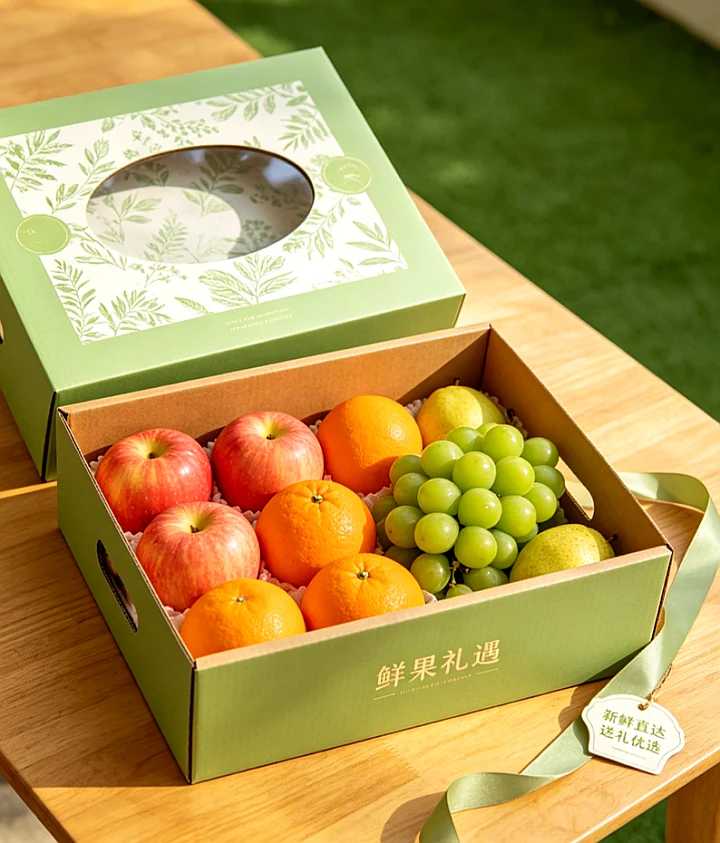
    Food-grade paper, grease-resistant liners and FSC board for tea tins, mooncakes and gift sets.

  • Apparel & accessories

    Hang tags, size cards and printed bags matched to the paper and finish used on the box.

  • Retail & display

    Counter display sets and portable display cards that ship flat and assemble without tools.

Follow the factory

Production runs, packing details and factory-floor clips are posted on these accounts. They are the channels we operate ourselves — any other account using the company name is not affiliated.

Questions buyers ask before sending a file

Can I order only 500 pieces for a first run?
Yes. 500 pcs per design is our standard minimum for rigid boxes, folding cartons and paper bags. Custom dies, inserts and foil blocks are tooling that has to be amortised — if your quantity falls below 500 we say so at quotation stage, not after sampling.
How are these cases put together?
They are compiled from our production records: press sheets, QC logs and the retained sample library. Client names stay confidential, so each case is described by product type, board grade, structure and quantity.
Can I reuse the parameters from a case?
Quote the case number in your enquiry. If your board, structure and finishing are close, we start from parameters that have already been proven instead of re-testing from scratch.
Do you sign NDAs and keep our artwork private?
Yes. We work under NDA on request, do not use client artwork in promotion without permission, and never publish client names.

Customer Reviews

Real feedback from packaging partners around the world

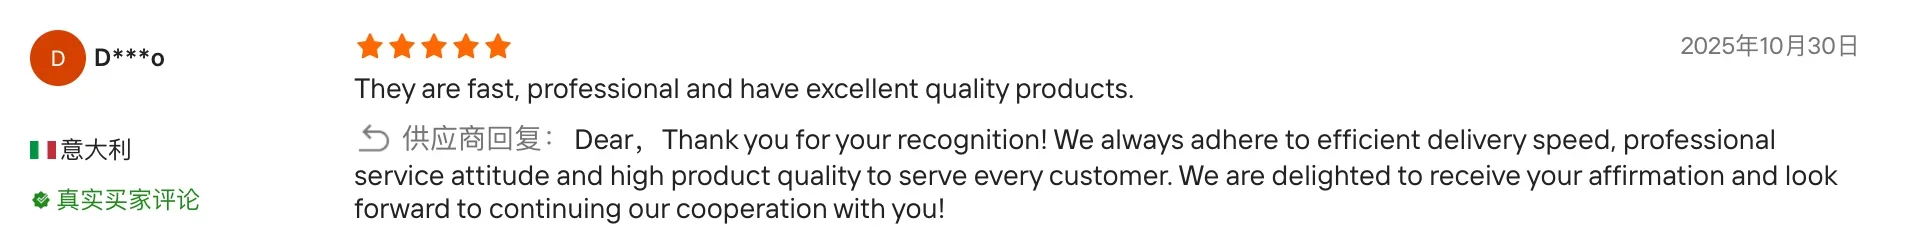
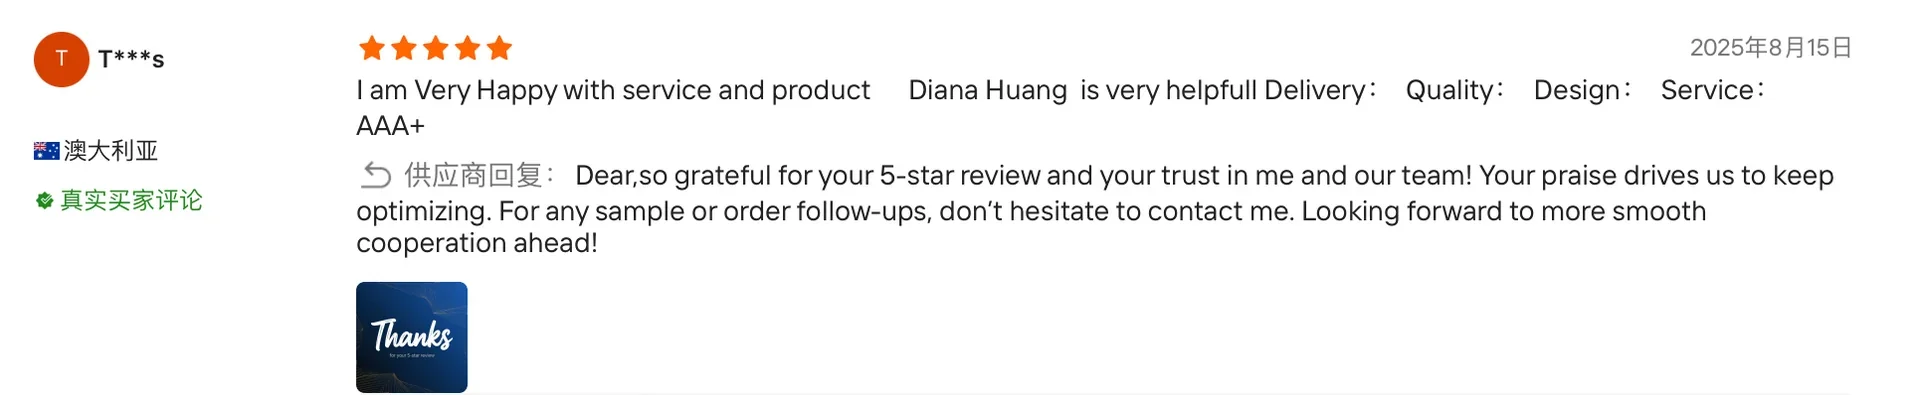
Customer review testimonial 1 - Zhengyang Packaging Dongguan China
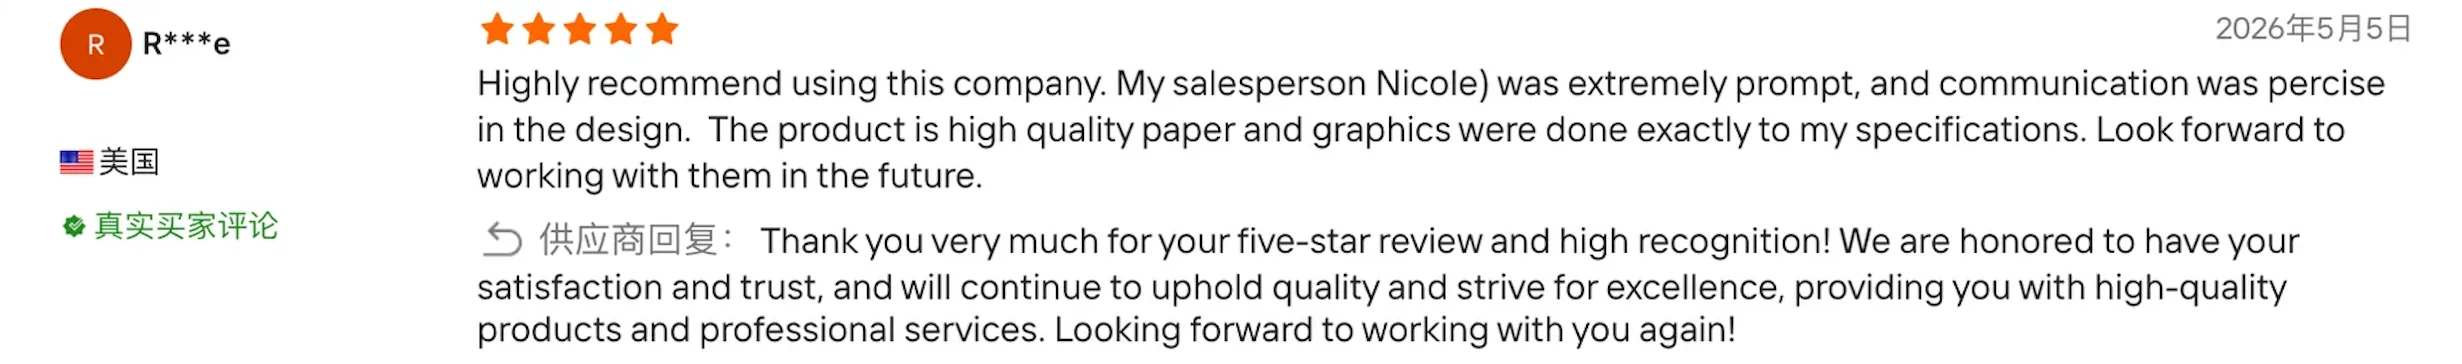
Customer review testimonial 3 - Zhengyang Packaging Dongguan China
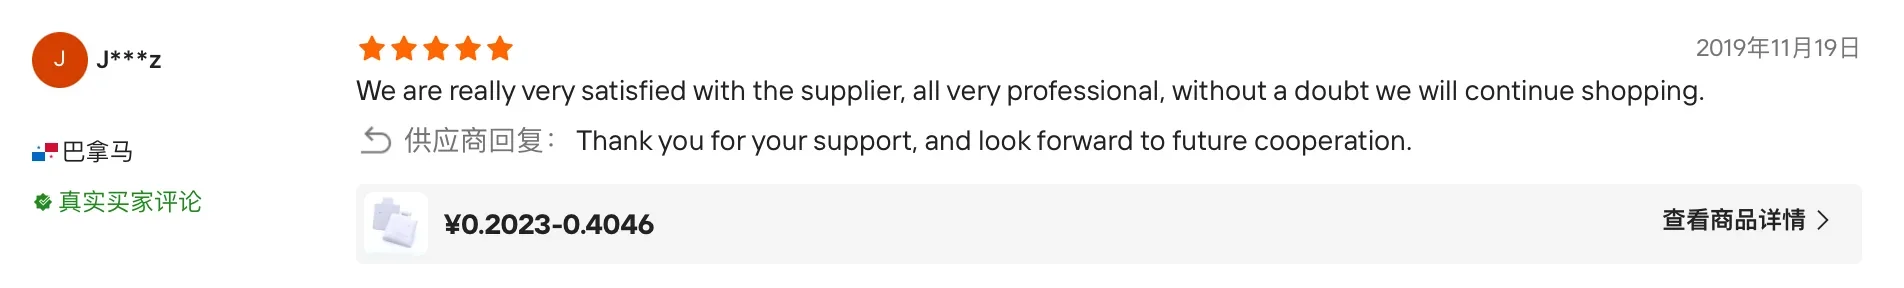
Customer review testimonial 4 - Zhengyang Packaging Dongguan China
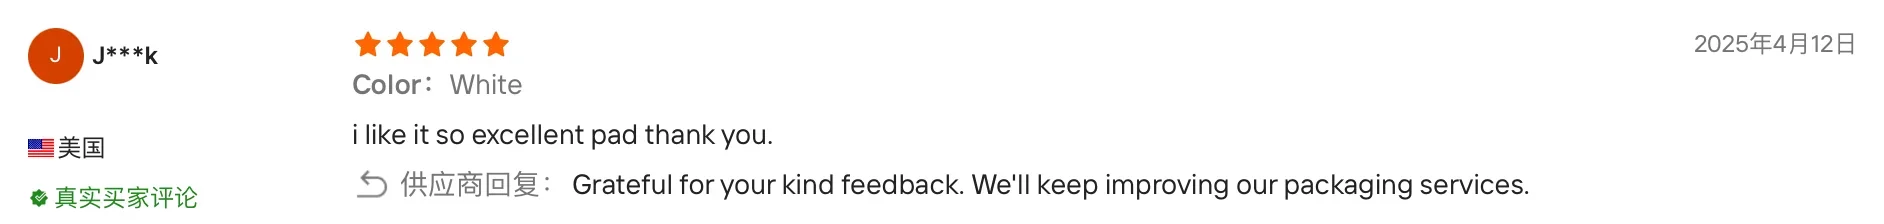
Customer review testimonial 5 - Zhengyang Packaging Dongguan China
Customer review testimonial 6 - Zhengyang Packaging Dongguan China
Customer review testimonial 7 - Zhengyang Packaging Dongguan China
Customer review testimonial 8 - Zhengyang Packaging Dongguan China
Customer review testimonial 9 - Zhengyang Packaging Dongguan China
Customer review testimonial 10 - Zhengyang Packaging Dongguan China
Customer review testimonial 11 - Zhengyang Packaging Dongguan China
Customer review testimonial 12 - Zhengyang Packaging Dongguan China
Customer review testimonial 13 - Zhengyang Packaging Dongguan China
Customer review testimonial 14 - Zhengyang Packaging Dongguan China
Customer review testimonial 15 - Zhengyang Packaging Dongguan China

Your project could be the next case

Send us your product, quantity and target market. We reply within 24 hours with structure suggestions, material options and a factory-direct quote.

💡 Try: gift box, carton, paper bag, hang tag, UV, foil...